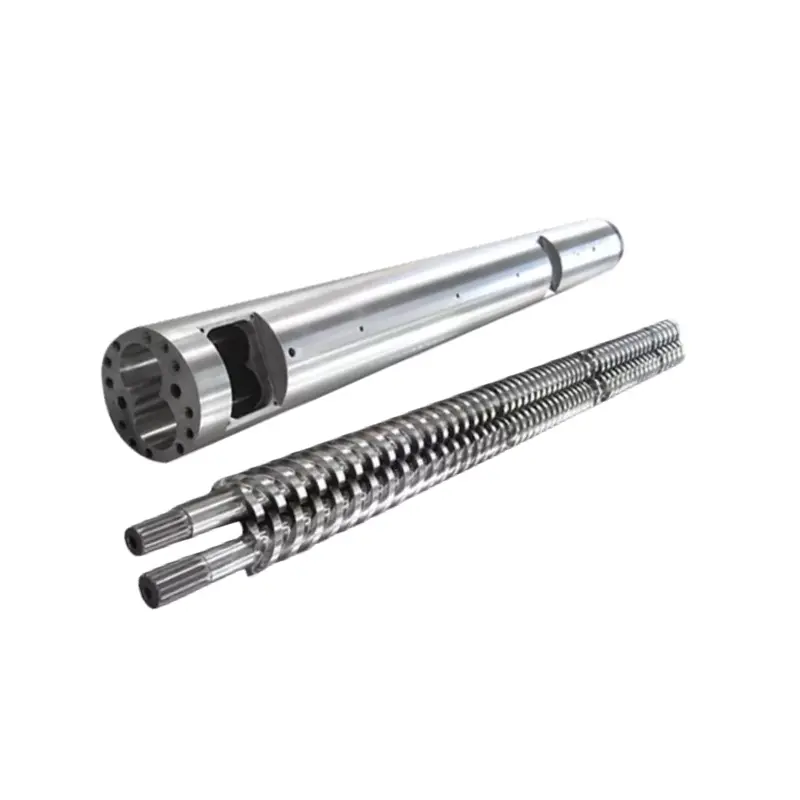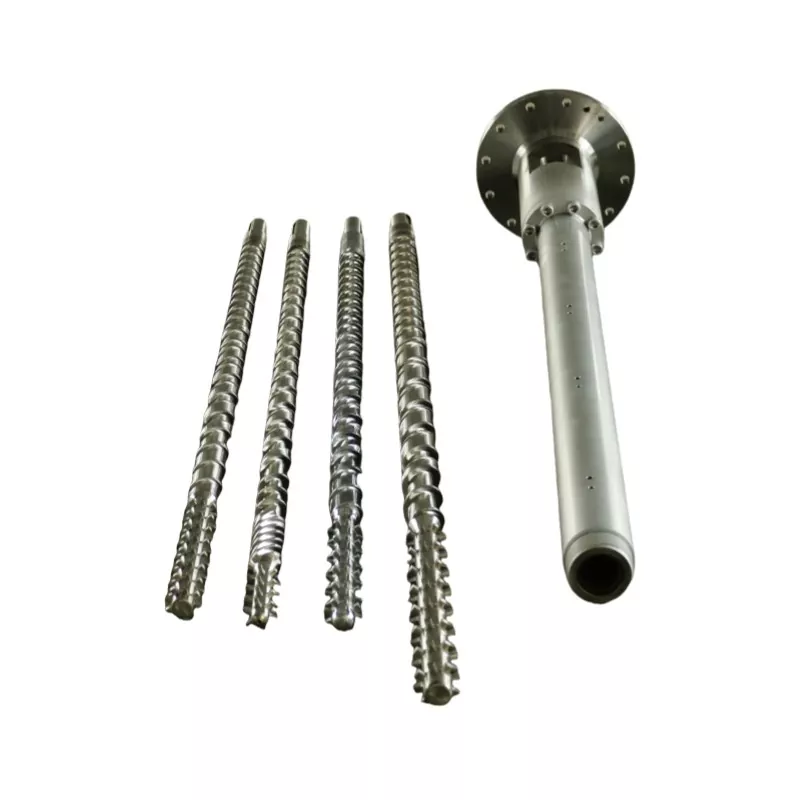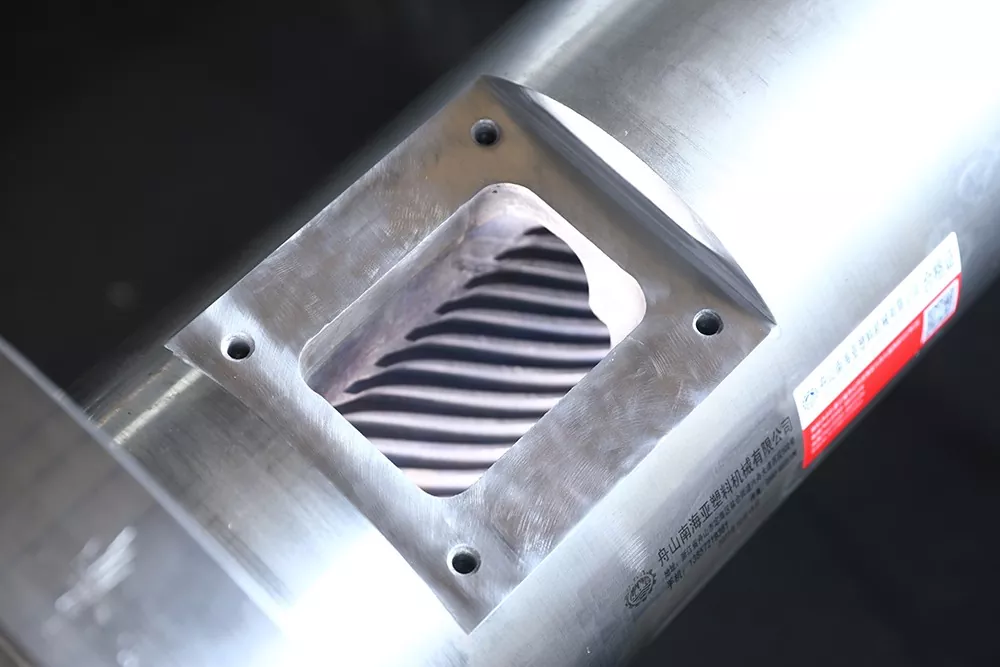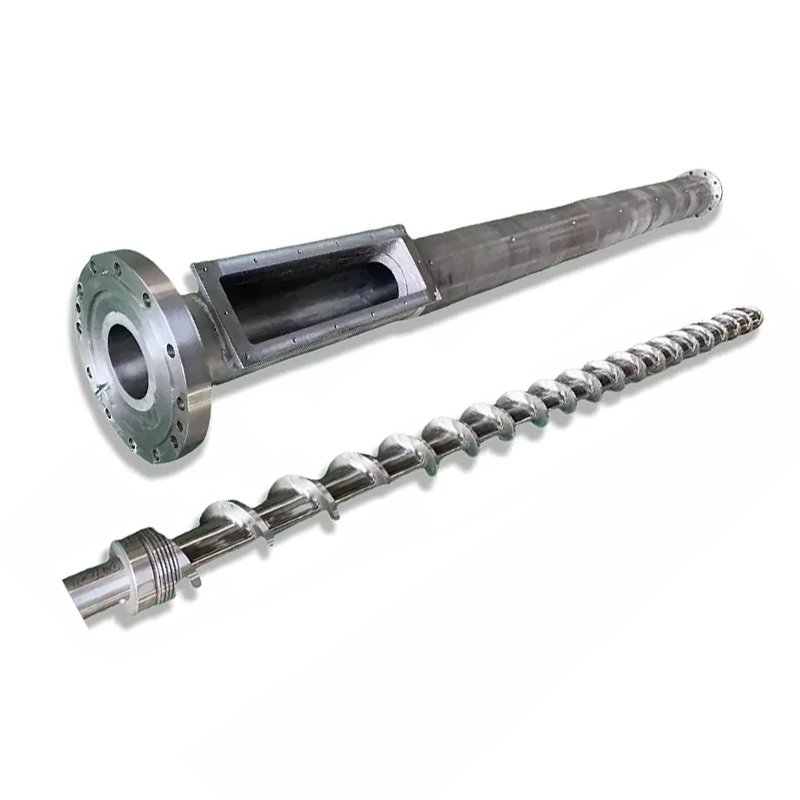

Qhov Screw chim tiag tiag ua
Cov ntsia hlau thiab lub thoob ua haujlwm ua ib khub. Nov yog cov kab ke txhua lub voj voog:
- Pub- Plastic pellets poob los ntawm lub hopper mus rau qhov chaw pub.
- Melting- Lub rotating ntsia hlau generates shear tshav kub. Ua ke nrog cov kav dej kub, pellets yaj thiab compress.
- Kev ntsuas- Cov yaj yuav zoo ib yam hauv qhov kub thiab txias ua ntej txhaj tshuaj.
- Txhaj tshuaj- Cov ntsia hlau txav mus rau pem hauv ntej zoo li lub plunger, thawb cov yas molten rau hauv pwm.
Txhua qhov kev tsim qauv sib txawv - geometry, thaj tsam proportions, kev kho saum npoo - cuam tshuam rau plaub kauj ruam zoo li cas. Ib qho kev tsis sib haum xeeb hauv ib qho ntawm lawv tshwm sim raws li qhov teeb meem tsim khoom.
Kev txiav txim 1: L/D Ratio
L / D piv (ntsia hlau dav dav faib los ntawm nws txoj kab uas hla) yog tus lej tseem ceeb tshaj plaws ntawm daim ntawv spec. Nws tswj lub sijhawm nyob, sib xyaw kom zoo, thiab kev faib hluav taws xob.Feem ntau cov hom phiaj txhaj tshuaj molding siv 20: 1.
| Resin | Pom zoo L/D |
|---|---|
| PP, PE, PS (tus qauv) | 18:1–20:1 |
| ABS, PC | 20:1-24:1-20 |
| PVC (kub-sensitive) | 16:1–20:1 |
| PET | 20:1–22:1 |
| Nylon (PA) | 18:1–20:1 |
| GF cov ntaub ntawv ntxiv | 20:1-24:1-20 |
Kev txiav txim siab 2: Compression Ratio
Qhov sib piv compression (CR) ntsuas ntau npaum li cas cov ntsia hlau channel nqaim los ntawm thaj chaw pub rau thaj tsam ntsuas. Siab dua CR compresses lub yaj ntau aggressively - zoo rau amorphous resins uas soften maj. Lower CR yog softer, uas yog qhov koj xav tau rau cov ntaub ntawv kub-sensitive lossis fiber ntau.
| Resin | Compression Ratio |
|---|---|
| ABS, PC, PMMA (amorphous) | 3.0–3.5: 1 |
| PP, PE, Nylon (semi-crystalline) | 2.5–3.0: 1 |
| PVC | 2.0–2.5: 1 |
| PET | 2.3–2.6:1 |
| GF-reinforced (≥15%) | 2.0–2.5: 1 |
Kev txiav txim siab 3: Thaj Av Loj
Ib tug txheej txheem txhaj ntswj faib ua peb cheeb tsam. Qhov kev faib ua feem ntawm txhua cheeb tsam tseem ceeb npaum li tag nrho L / D.
- Pub Zone (L1):Cov kab sib sib zog nqus uas txais cov khoom pellets los ntawm lub hopper. Ntev = ntau lub peev xwm dhau los.
- Compression Zone (L2):Channel qhov tob txo qis zuj zus. Feem ntau ntawm melting tshwm sim ntawm no.
- Kev ntsuas thaj tsam (L3):Yooj yim, sib xws channel. Xyuas kom lub cev kub thiab siab ua ntej txhaj tshuaj.
| Resin | Pub (L1) | Compression (L2) | Kev ntsuas ntsuas (L3) |
|---|---|---|---|
| PP / PE | 50% | 25% | 25% |
| ABS / PC | 40% | 40% | 20% |
| PET | 40% | 40% | 20% |
| Nylon (PA) | 35-45% | 35-40% | 20-25% |
| PVC | 35% | 50% | 15% |
Kev Txiav Txim 4: Cov Khoom Siv Ntsia Hlau
38CrMoALA — Tus Qauv Txheej Txheem
Nanhaiya txhaj tshuaj molding screws yog tsim los ntawm38CrMoALA alloy hlau, kub-kho thiab quenched. Cov khoom siv hauv paus no tswj cov txheej txheem thermoplastics xws li PE, PP, PS, thiab ABS zoo, nrog rau kev pab cuam lub neej ntawm kwv yees li.10,000-20,000 teevnyob rau hauv ib txwm ua hauj lwm tej yam kev mob.
Nitriding
Gas nitriding ntawm 500-560 ° C tsim ib txheej nitrided0.5-0.8mm tuabnrog hardness ntawm950-1050 HV (~ 62 HRC). Qhov no txhim kho hnav tsis kam los ntawm 30-40% piv rau cov hlau tsis kho. Txuj rau feem ntau cov ntawv thov kev txhaj tshuaj molding khiav tsis tau puv lossis cov ntaub ntawv me me.

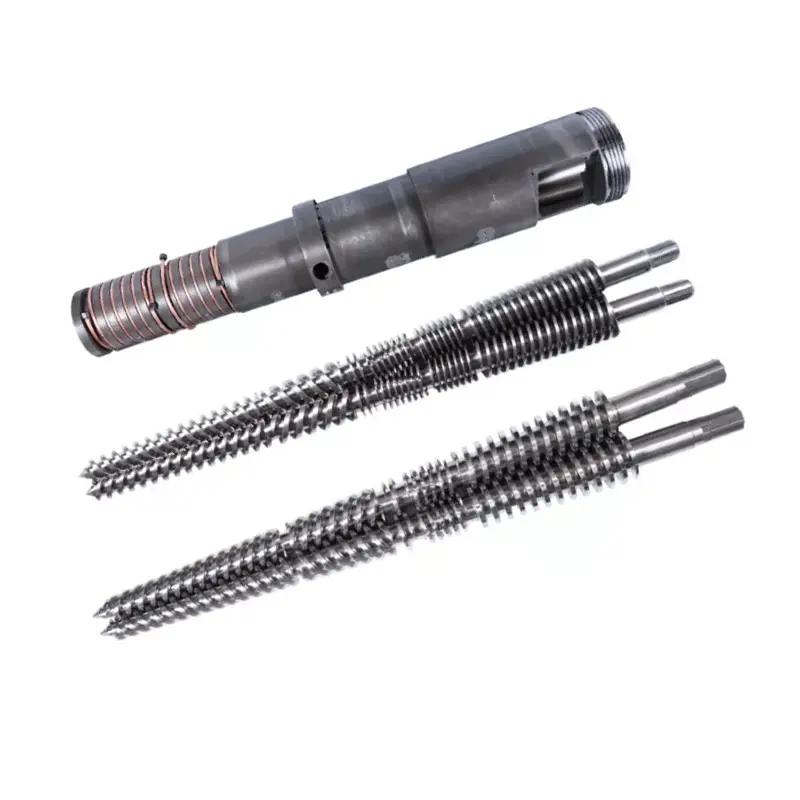
Nanhaiya mutant (abrupt) txhaj tshuaj molding ntsia hlau - haum rau crystalline resins zoo li PP, PE, thiab Nylon.
Bimetallic - Rau Abrasive Applications
Bimetallic chims muaj ib tug high-alloy hnav-resistant hauv ob sab phlu metallurgically bonded rau lub chim bore. Nanhaiya's bimetallic txheej txheem ua tiav ib qhoSab hauv bore hardness ntawm 62 HRClos ntawm cov tawv alloy tshuaj tsuag welding nyob ib ncig ntawm lub siab coj qhov chaw ntawm lub thoob sab hauv.
| Daim ntawv thov | Ntsia Hlau Khoom | Kev kho lub thoob |
|---|---|---|
| PE, PP, PS (tsis muaj) | 38CrMoALA nitrided hmoov | Txheem nitrided |
| ABS, PC, Nylon (tsis muaj) | 38CrMoALA nitrided hmoov | Txheem nitrided |
| PA + GF ≤ 30% | 38CrMoALA, quenched + tempered | Nitrided los yog bimetallic |
| GF cov ntsiab lus 15-50% | Bimetallic / TC davhlau ntug | Bimetallic |
| PVC / corrosive resins | Corrosion-resistant alloy | Bimetallic (CR qib) |
| Carbon fiber ntau | Tungsten carbide | TC-sprayed bore |
Kev txiav txim siab 5: Screw Diameter thiab txhaj tshuaj loj
Koj qhov kev txhaj tshuaj tiag tiag yuav tsum poob ntawm35% thiab 70%ntawm cov ntsia hlau qhov siab tshaj plaws txhaj tshuaj muaj peev xwm. Hauv qab 35%, cov khoom zaum hauv lub thoob ntev dhau lawm thiab muaj kev pheej hmoo degradation. Tshaj li 70%, cov ntsia hlau tsis tuaj yeem rov qab sai txaus hauv lub voj voog.
Hauv qab no yog cov configurations uas muaj los ntawm Nanhaiya:
| Tus nqi txhaj tshuaj (g) | Ntsia Hlau Ø × Length (mm) | Ø × Length (mm) |
|---|---|---|
| 30–90 : kuv | Φ30 × 900 | 85 × 860 hli |
| 60–125 : kuv | 35 × 910 hli | 85 × 860 hli |
| 100–150 | 38 × 935 hli | 95 × 900 hli |
| 125-300 Nws | 42 × 1030 hli | Φ105 × 1110 |
| 250-400 Nws | Φ45 × 1210 | Φ115 × 1165 |
| 300-500 | Φ50 × 1300 | Φ125 × 1260 |
| 500-700 | Φ60 × 1380 | Φ140 × 1350 |
| 700-1000 Nws | 70 × 1790 hli | Φ160 × 1685 |
| 1000-1500 | Φ160 × 3500 | Φ270 × 3200 |
| 1300-2500 Nws | Φ170 × 3415 | 317 × 3380 hli |

Nanhaiya maj mam txhaj tshuaj molding ntsia hlau - zoo dua rau amorphous resins xws li ABS, PC, thiab PMMA.
Kev ceeb toom qhia tias koj tus ntsia hlau tam sim no tsis raug rau txoj haujlwm
- Dub specks los yog hlawv cov cim- Cov khoom degrading los ntawm lub sij hawm nyob ntau dhau los yog qhov chaw kub. Txheeb xyuas qhov kub ntawm qhov chaw thiab cov ntsia hlau tshem tawm.
- Inconsistent txhaj tshuaj hnyav- Feem ntau ib qho hnav tsis rov qab los yog cov ntsia hlau ntau dhau-rau- chim tshem tawm tso cai rov qab.
- Splay cov cim rau ntawm qhov chaw- Moisture los yog roj nyob rau hauv lub yaj. Tej zaum yuav qhia tau tias tsis txaus ua ntej ziab los yog lub hau ntswj geometry uas tsis yog qhov cua zoo.
- Rov qab qeeb / lub sij hawm mus sij hawm ntev- Plasticizing muaj peev xwm tsis txaus. Screw txoj kab uas hla yuav tsum tau nce.
- Siab khawb ntawm cov xim hloov- Kev sib xyaw tsis zoo hauv thaj chaw ntsuas ntsuas. Lub Maddock lossis barrier mixing ntsiab ntxiv rau cov ntsia hlau feem ntau daws qhov no.
Yuav Qhia Li Cas Rau Koj Tus Neeg Tsim Khoom Thaum Thov Kev Tso Cai
- Tshuab hom thiab qauv- los yog bore txoj kab uas hla thiab flange qhov ntev rau cov tshuab tsis-tus qauv
- Primary resin (cov)- suav nrog hom muab tub lim thiab feem pua yog tias muaj
- Kev txhaj tshuaj ntau yam- yam tsawg kawg nkaus thiab siab tshaj hauv grams
- Lub hom phiaj lub sij hawm voj voog
- Cov teeb meem tam sim no koj tab tom sim daws— yog muaj
Tau txais kev pom zoo los ntawm Nanhaiya
Peb teb hauv 12 teev. Peb pab neeg ua haujlwm engineering tuaj yeem hais qhia txog txoj cai ntswj geometry, qib khoom, thiab qhov ntev rau koj lub tshuab thiab cob - ua ntej koj cog lus rau ib qho kev tsocai.