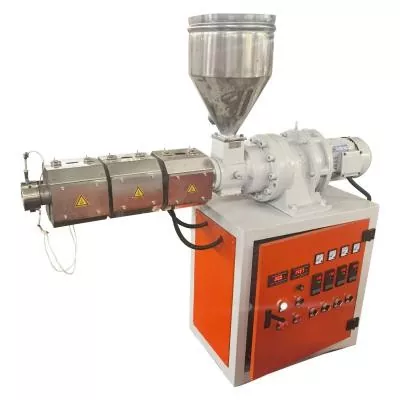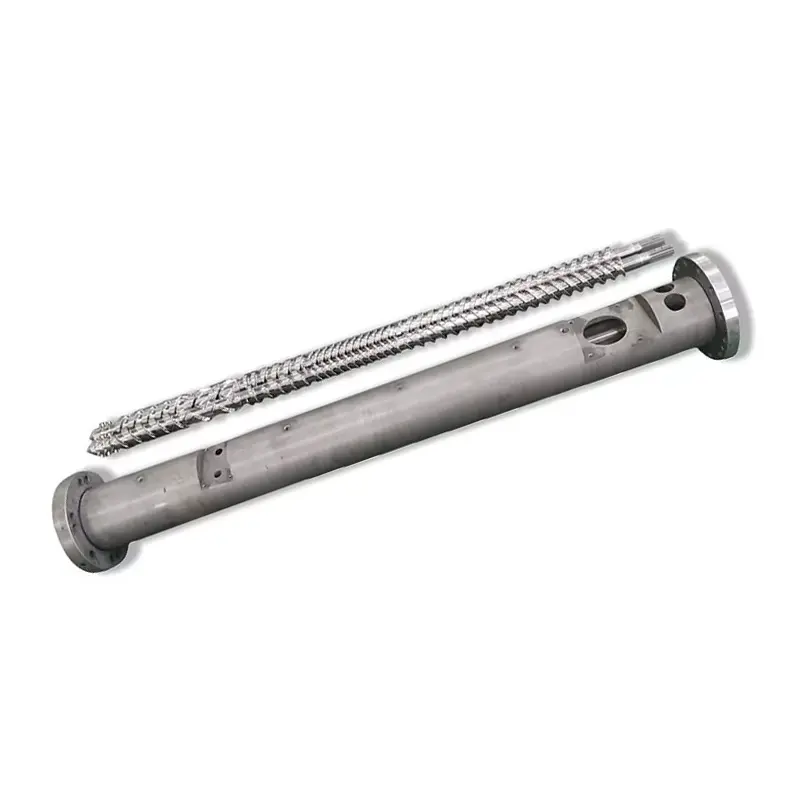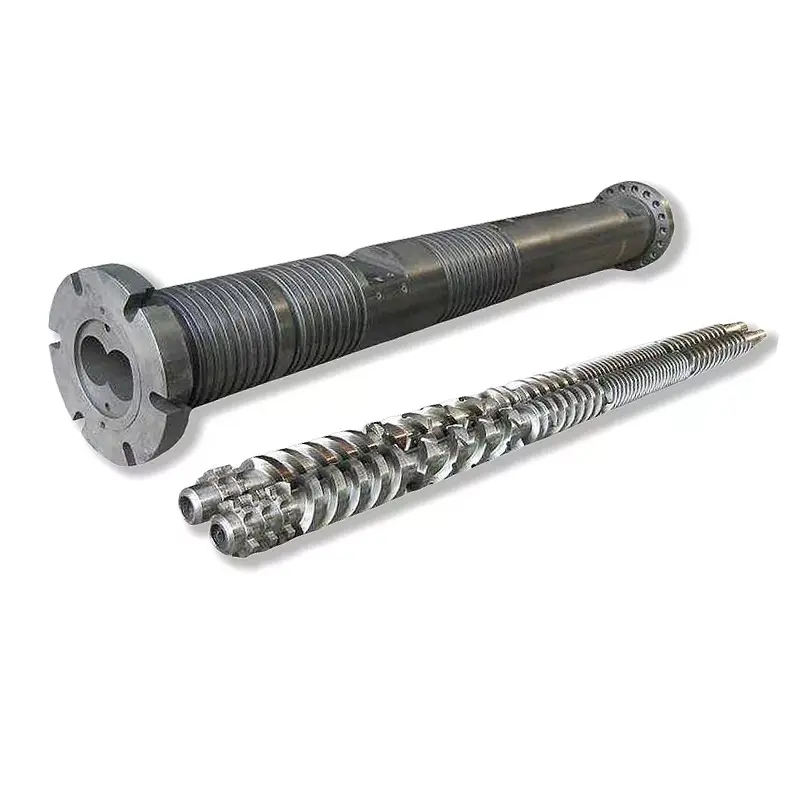
Lub sijhawm rov qab qeeb tuaj yeem taw tes rau qhov teeb meem pub mis, hloov txheej txheem lossis cov khoom siv hnav. Qhov kev kuaj mob muaj txiaj ntsig qhia koj tias qhov twg yog qhov twg, thiab seb nws puas ua rau koj lub sijhawm mus ncig.
Yog tias txhaj tshuaj molding ntsia hlau rov qab siv sijhawm ntev heev, thawj zaug paub meej tias nws ncua lub voj voog. Tom qab ntawd xyuas cov khoom noj txuas ntxiv, qhov tseeb ntsia hlau ceev, rov qab siab thiab qhov kub thiab txias tiv thaiv kev ua haujlwm ruaj khov. Tshawb xyuas geometry thiab hnav thaum cov tshev no tsis piav qhia qhov poob. Hloov cov khoom siv tsuas yog tom qab txheeb xyuas qhov txwv kev ua haujlwm.

Ua ntej, tsim kom muaj kev rov qab los ntawm lub voj voog txoj hauv kev tseem ceeb
Screw rov qab yog lub plasticizing thiab metering theem: cov ntsia hlau rotates, npaj cov tshuaj tom ntej thiab retracts li yaj accumulates nyob rau hauv pem hauv ntej ntawm nws. Nws txawv ntawm kev txhaj tshuaj, thaum cov ntsia hlau txav mus rau pem hauv ntej kom xa qhov txhaj tshuaj ntawd. Tshawb xyuas koj tus maub los lub sijhawm txhais, tshwj xeeb yog tias nws suav nrog kev ncua lossis decompression.
Kev rov qab feem ntau cuam tshuam ib feem ntawm qhov ua kom txias txias. Nws cov nyhuv ntawm tag nrho lub sij hawm lub voj voog yog li ntawd nyob ntawm seb thaum rov qab pib thiab lub tshuab ua haujlwm twg yuav tsum tau tos kom tiav. Nyeem cov kab ke ib ntus es tsis xav tias txhua thib ob raug tshem tawm los ntawm kev rov qab tshem tawm ib qho thib ob ntawm lub voj voog.
| Lub sijhawm rov qab los | Tos dhau lub qhov rais | Qhov kev hloov no txhais li cas |
|---|---|---|
| 12 vib nas this | 2 vib nas this | Kev rov qab los ncua kev ua haujlwm tom ntej. |
| 9 nqi | 0 vib nas this | Qhov kev txhim kho 3-thib ob rov qab tshem tawm 2 vib nas this ntawm kev tos. |
| 7 vib nas this | 0 vib nas this | Lwm 2 vib nas this tawm rov qab coj tsis tau ntxiv lub voj voog txo qis hauv qhov piv txwv no. |
Peb thawj lo lus nug yog seb lub tshuab puas yog tos kom yaj lossis tsuas yog qhia tus lej koj xav txo. Yog tias qhov rov qab tau zoo nyob rau hauv lub qhov rais muaj, peb yuav tsom mus rau qhov sib xws thiab yaj zoo ua ntej pom zoo rau cov khoom siv ntau dua.
Rau kev piav qhia dav dav ntawm lub rooj sib txoos, saib pebtxhaj tshuaj molding ntsia hlau chim qhia. Ntawm no, lub hom phiaj yog nqaim dua: tsim kom muaj vim li cas rov qab hloov pauv thiab ua dab tsi cov pov thawj txhawb nqa.
Kev hloov tam sim ntawd thiab kev poob qis yuav tsum muaj cov ntsiab lus pib sib txawv
Txuag ib qho kev siv ua ntej kho lub tshuab. Sib piv tib qib resin, regrind piv, qhov chaw txhaj tshuaj, pwm thiab qhov kub thiab txias. Sau tus kheej mus raws li qhov nruab nrab; ib qho kev rov qab qeeb qeeb tuaj yeem cuam tshuam kev tsim khoom txawm tias qhov nruab nrab zoo li tau txais.
| Pom qauv | Tshawb xyuas ua ntej | Cov ntaub ntawv pov thawj tsim nyog sau cia |
|---|---|---|
| Sudden nce tom qab hloov cov ntaub ntawv los yog daim ntawv qhia | Pub daim ntawv, regrind, qhuav mob thiab hloov chaw | Cov khoom siv ntau, sib tov piv, particle mob thiab ua ntej / tom qab txheej txheem cov ntaub ntawv |
| Cov voj voog qeeb qeeb nrog cov voj voog ib txwm nyob nruab nrab ntawm lawv | Pub cuam tshuam, kev sib txuas thiab kev hloov pauv ceev | Rov qab taug qab, kev ua haujlwm loader thiab RPM tiag tiag rau tib lub voj voog |
| Kev rov ua kom rov zoo zuj zus zuj zus nyob rau hauv lub luag haujlwm ruaj khov | Txheeb xyuas cov xwm txheej ua haujlwm, tom qab ntawd tshuaj xyuas qhov hnav | Cov ntaub ntawv keeb kwm rov qab thiab ntsuas cov ntsia hlau / thoob qhov ntev |
| Siab load thiab tiag RPM hauv qab cov lus txib | Tshuab tsav, torque txwv thiab thermal mob | Qhov tseeb tiv thaiv tau hais kom RPM, thauj khoom sib txawv thiab lub tswb tshuab |
| Teeb meem pib tam sim ntawd tom qab hloov cov khoom | Nruab ib feem tus kheej, qhov ntev, geometry thiab sib dhos | Pom zoo kos duab kho dua tshiab, haum cov khoom siv thiab kev teeb tsa commissioning |
Cov qauv no txiav txim siab qhov kev soj ntsuam; tsis muaj pov thawj los ntawm nws tus kheej. Kev ua txhaum sai sai nrog lub suab nrov, kev sib tw lossis kev thauj khoom tsis zoo yuav tsum tau ceev lub tshuab-kev pabcuam, txawm tias lub sijhawm pib zoo li cov txheej txheem teeb meem.
Paub meej tias cov pellets ncav cuag cov ntsia hlau tsis tu ncua
Lub hopper tag nrho tsis tsim kom muaj cov ntsia hlau tau noj. Xyuas lub loader, shutoff swb, cov ntaub ntawv txoj kev thiab pub-caj pas txias. Nrhiav ib qho kev cuam tshuam uas coincides nrog lub voj voog qeeb ua ntej hloov qhov compression seem lossis xaj ib lub hau ntswj tshiab.
Asahi KaseiAsaclean kev taw qhia ntawm kev pub- caj pas bridgingpiav qhia yuav ua li cas thaum tshav kub kub nyob ze ntawm lub rear chim cheeb tsam yuav soften pellets ntxov ntxov. Cov pellets tuaj yeem clump thiab cuam tshuam txoj kev, tawm hauv cov ntsia hlau luv ntawm cov khoom txawm tias resin tseem nyob saum nws.
Txheeb xyuas qhov hloov pauv hauv qhov pub nws tus kheej. Ib qho sib txawv regrind piv, ntau nplua los yog cov khoom tsis xwm yeem tsim nyog saib xyuas. Celanese tshwj xeeb txuas rov ua qhov zoo rau kev noj zaub mov thiab rov qab teeb meem hauv nwsVectra® LCP phau ntawv qhia. Nws cov lus pom zoo yog cov khoom siv tshwj xeeb, tab sis lawv muab cov laj thawj tseem ceeb los sau cov xwm txheej tsis yog lub npe resin xwb.
Yog tias qhov rov qab tsis zoo tom qab hloov pauv, peb yuav muab piv nrog cov ntawv pom zoo siv ua ntej hloov kho vajtse. Yog tias qhov kev coj cwj pwm qub rov qab los, qhov kev tshawb nrhiav pub tau txais qhov tseem ceeb. Qhov txiaj ntsig ntawd ua rau lub Hoobkas muaj kev coj zoo dua li qhov kev thov rau "ntse ceev dua."
Kev ziab tseem yuav tsum tau ua kom tau raws li tus neeg xa khoom xav tau. Tsis txhob xav tias cov dej noo yog qhov piav qhia rau txhua qhov teeb meem ntawm lub sijhawm, lossis qhov kev pom zoo rov qab ua pov thawj tias cov resin qhuav txaus. Kev ua tau zoo thiab qhov kawg ntawm qhov zoo yuav tsum tau kuaj xyuas nyias.
Txheeb xyuas qhov ceev ceev, rov qab siab thiab yaj kub ua ke
Nyeem qhov RPM tiag tiag, tsis yog qhov teeb tsa xwb
Yog tias cov lus txib tsis hloov pauv tab sis cov ntsia hlau tig qeeb dua, tshawb xyuas lub tshuab ua haujlwm txwv thiab tsav tus cwj pwm. Cov lus pom zoo geometry tsis tuaj yeem daws qhov tsis tau piav qhia ntawm qhov kev thov thiab xa nrawm. Sau qhov tseeb ceev los ntawm kev rov qab mob stroke, tshwj xeeb tshaj yog qhov pib qeeb.
RPM kuj xav tau lub taub hau taub hau kom txhais tau ntau. Pebtxhaj tshuaj molding ntsia hlau ntausuav nrog txoj kab uas hla ntawm 30 mus rau 170 mm. Hloov qhov kev sib hloov-ceev qhov chaw ntawm qhov sib txawv diameters hloov lub peripheral ceev ntawm cov ntsia hlau nto.
Peripheral ceev, m / s = π × inch, mm × RPM ÷ 60,000
Ntawm 100 RPM, 40 mm ntsia hlau muaj qhov ceev ntawm qhov nruab nrab ntawm 0.209 m / s; 60 hli ntsia hlau ncav cuag li 0.314 m/s. Cov no yog cov piv txwv suav, tsis pom zoo rau kev teeb tsa lossis kev suav ncaj qha ntawm yaj shear tus nqi.
Siv cov qib resin tiag tiag cov txheej txheem kev taw qhia thiab lub tshuab txwv kom txiav txim siab ceev. Kev nce RPM yog qhov tseem ceeb tsuas yog tias lub tshuab tuaj yeem xa nws thiab qhov tshwm sim yaj tseem tuaj yeem siv tau.
Nrhiav seb yog vim li cas lub siab rov qab tau teem rau qhov twg
Rov qab siab tiv thaiv cov ntsia hlau tawm thaum lub sijhawm rov qab los thiab cuam tshuam li cas cov khoom siv plasticized. Yog tias nws tau nce los kho qhov sib xyaw lossis ntsuas kev txhawj xeeb, txo nws yooj yim los txhim kho lub sijhawm tuaj yeem coj qhov teeb meem zoo rov qab. Paub meej tias seb lub siab tso tawm yog hydraulic lossis lub siab yas tshwj xeeb ua ntej sib piv cov cav tov.
Ib qho kev pom zoo rau kev txhawb nqa rov qab thoob ntiaj teb yog qhov tsis muaj txiaj ntsig tshwj xeeb. Rau Vectra LCP,Celanese qhia qhov tsawg kawg nkaus rov qab siab, 5-15 bar tshwj xeeb, thiab ceeb toom txog overheating thiab fiber ntau puas ntsoog. Qhov ntawd yog kev taw qhia rau Vectra, tsis yog qhov chaw rau luam rau hauv PP, ABS lossis PC txheej txheem.
Tshawb xyuas lub yaj ua ntej lees txais qhov chaw nrawm dua
Barrel setpoints tsis qhia tag nrho cov thermal mob ntawm cov yaj. Ua raws li cov txheej txheem ntsuas qhov ntsuas kub tau pom zoo, txheeb xyuas lub tshuab cua sov thiab ntsuas qhov ntsuas, thiab sib piv ib feem zoo tom qab kev hloov pauv. Lub sij hawm rov qab luv dua nrog cov xim tsis zoo, cov khoom siv tsis sib xws lossis tsis zoo sib xws tsis yog qhov ua tiav tiav.
Hloov ib qho kev sib txawv ntawm ib lub sij hawm thiab tso cai rau cov txheej txheem kom ruaj khov. CovVectra teeb meem kev taw qhiasiv tib theem kev mus kom ze. Khaws qhov kev sim rau hauv lub qhov rais ua haujlwm pom zoo rau cov khoom koj tau khiav.
Cais ib seem conveying hnav los ntawm lub nplhaib checking
Thaum pub mis thiab kev ua haujlwm zoo sib piv tab sis kev rov qab ua kom tsis zoo, qhov xwm txheej ntawm cov ntsia hlau thiab lub thoob tsim nyog tau txais kev tshuaj xyuas. Ntsuas lub davhlau sab nraud txoj kab uas hla thiab lub thoob bore ntawm txoj hauj lwm uas tau teev tseg los ntawm kev kos duab los yog tsim cov kev txwv. Tshawb xyuas qhov kev puas tsuaj raws li qhov ntev.
Cov ntsia hlau-pem hauv ntej sib dhos xav tau kev sim sib txawv. Thaum rov qab los, lub valve tsis rov qab tso cai rau yaj mus rau pem hauv ntej; Thaum lub sij hawm txhaj tshuaj, nws yuav tsum muab khi tiv thaiv rov qab ntws. Lub valve xau tuaj yeem cuam tshuam qhov sib xws ntawm kev txhaj tshuaj, tab sis qhov ntawd tsis tsim kom ntseeg tau tias cov ntsia hlau yas seem tau hnav tawm.


Yog hais tias lub cushion lossis txhaj tshuaj hnyav kuj txawv, suav nrog lub tshuab tsim cov khoom tsis rov qab-valve test hauv kev tshawb nrhiav. Pebntsia hlau tip xaiv phau ntawv qhianpog lub nplhaib, lub rooj zaum thiab mating qhov ntev hauv kev nthuav dav ntxiv.
Peb yuav tsis tso cai ua kom tiav cov ntsia hlau-thiab-thooj hloov ntawm lub sijhawm qeeb ib leeg. Conversely, ib tug tshiab ntsia hlau yuav tsum tsis txhob mus rau hauv ib tug hnav chim chim yam tsis tau kuaj xyuas qhov tshwm sim haum. Nug rau ib daim ntawv qhia qhov ntev uas txheeb xyuas cov haujlwm ntsuas thiab cov kev txwv coj los siv kom ncav cuag qhov kev pom zoo.
Thaum twg tus ntsia hlau txawv tsim ua rau kev nkag siab?
Kev tshuaj xyuas tus qauv tsim muaj txiaj ntsig zoo thaum lub geometry tam sim no tsis tuaj yeem ua tau raws li lub luag haujlwm xav tau hauv kev ua haujlwm tau zoo. Qhov no yuav ua raws li kev hloov pauv, qhov yuav tsum tau txhaj tshuaj loj dua lossis luv dua qhov rov qab muaj qhov rai. Khaws nws cais los ntawm kev rov ua kom cov txheej txheem ua tiav yav dhau los uas tau yooj yim deteriorated.
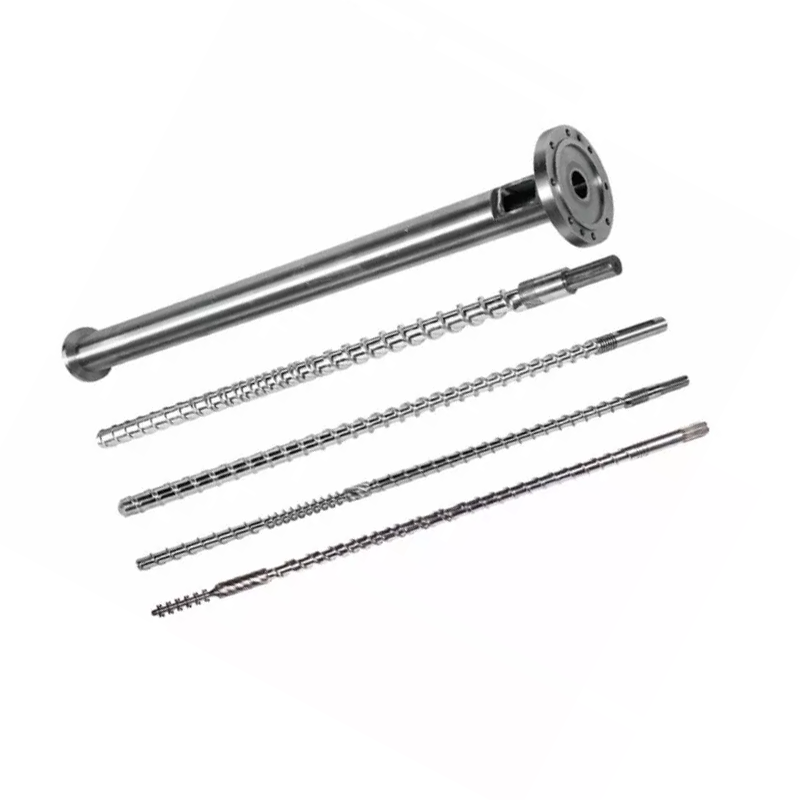
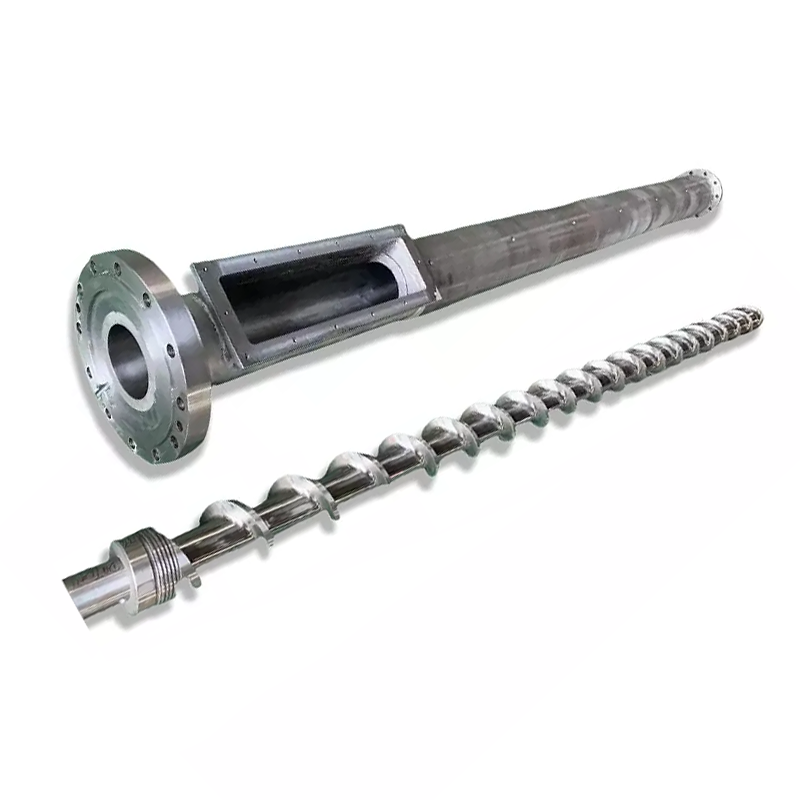
Peb ob qhov kev txhaj tshuaj ntsia hlau khoom tsev neeg qhia txog kev xaiv tsim tsim:
| Nanhaiya design | Compression seem | Peb yuav siv nws li cas hauv kev tshuaj xyuas |
|---|---|---|
| Maj mam txhaj molding ntsia hlau | Feem ntau 40% -60% ntawm tag nrho cov ntsia hlau ntev, kwv yees li 50% ntawm cov khoom piav qhia | Ib tug ntev, maj mam txo nyob rau hauv channel qhov tob rau lub luag hauj lwm uas yuav tsum tau tswj plasticization. Ntsuam xyuas qhov tseeb resin, txhaj tshuaj thiab thermal cwj pwm. |
| Mutant txhaj molding ntsia hlau(abrupt-compression design) | Kwv yees li 5% -15% ntawm tag nrho cov ntsia hlau ntev | Kev hloov pauv luv dua nrog kev txo qis hauv qhov tob ntawm channel. Ntsuas lub luag haujlwm melting thiab thermal uniformity ua ntej xaiv nws los daws qhov muaj peev xwm txwv. |
Peb maj mam tsim npog cov ntawv thov xws li PS, PC thiab ABS; tsev neeg abrupt-compression suav nrog cov ntawv thov xws li PE thiab PP. Cov kev tsim khoom no pab pib kev sib tham. Lawv tsis hloov cov resin-qib thiab tshuab tshuaj xyuas, tshwj xeeb tshaj yog nrog cov fillers, regrind los yog xav tau kev qhia zoo.

Kev kho qhov chaw nyob qhov chaw hnav, tsis yog thaiv caj pas
Ob tsev neeg cov khoom siv 38CrMoAlA steel. Lawv cov khoom lag luam-cov ntsiab lus nthuav dav suav nrog cov kev xaiv kho mob hauv qab no, uas muaj nyob rau hauv kev sib tham hloov pauv thaum kev tshuaj xyuas txheeb xyuas qhov hnav:
| Khoom | Cov khoom lag luam-tus nqi nthuav dav | Nws txhais li cas rau kev nug |
|---|---|---|
| Nitriding hardness | HV900-1100 | Qhia qhov chaw kho mob thiab tshuaj xyuas yuav tsum tau ua. |
| Nitriding qhov tob | 0.5-0.8 hli | Txheeb xyuas qhov kev kho mob xaiv; tsis txhob xav txog kev pabcuam lub neej los ntawm qhov tob ib leeg. |
| Nickel-tungsten alloy hardness | HRC55-62 | Tshawb xyuas cov hlau nrog cov khoom siv tiag tiag, muab tub lim thiab hnav qauv. |
| Alloy txheej qhov tob | 0.8-2.0 hli | Txhais cov cheeb tsam ntxiv rau ntawm qhov pom zoo cov ntsiab lus tshwj xeeb. |
Pebgradual ntsia hlau khoom cov ntsiab luspiav qhia txog kev txhawb nqa ntawm cov chaw tsis muaj zog nrog nickel-tungsten alloy. Los ntawm kev pom ntawm lub Hoobkas, peb xav kom muaj kev tiv thaiv kev tiv thaiv raws li kev ntsuas coj los ntsuas. Ib qho chaw kim dua tsis kho qhov tsis txaus noj lossis tsim kom muaj cov ntsia hlau geometry haum rau cov resin.


Tig qhov kev kuaj mob mus rau ib qho tshwj xeeb
Khaws cov lus pom zoo kom nqaim raws li cov pov thawj tso cai. Ib qho kev cuam tshuam kev noj zaub mov hu rau kev kho qhov kev noj zaub mov. Cov lus txib ceev lub tshuab tsis tuaj yeem tuav hu rau lub tshuab tshuaj xyuas. Kev lees paub lub valve xau hu rau lub valve thiab kev ntsuam xyuas interface. Ntsuas cov ntsia hlau los yog lub taub hau hnav txhawb nqa ib qho kev hloov khoom siv lossis kev ntsuam xyuas tsim nyog.
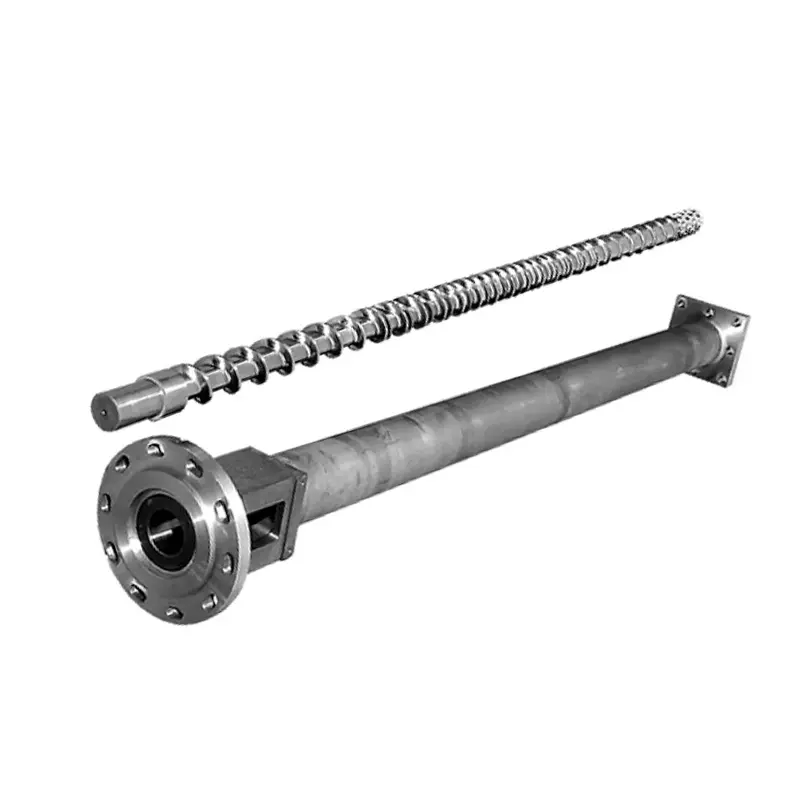
Yog hais tias lub rooj sib txoos yog nyob rau hauv qhov kev lees paub tab sis lub luag haujlwm tsim khoom tshiab tshaj nws lub peev xwm plasticizing, xa cov qauv luv luv. Nanhaiya muab kev cai ntsia hlau tsim, machining thiab alloy tshuaj tsuag vuam. Pebcov khoom siv ntau lawmsuav nrog CNC lathes rau workpieces txog li 6 meters ntev thiab tsib-axis machining rau complex flights thiab flange lug.

Xa cov ntaub ntawv uas piav qhia txog qhov teeb meem
- Tshuab tsim thiab qauv, ntsia hlau txoj kab uas hla, sib dhos daim duab thiab haum cov ntsiab lus ntawm cov ntsia hlau.
- Resin qib, muab tub lim loading, regrind ratio thiab particle condition.
- Lub sijhawm rov qab los ntawm lub voj voog, qhov tseeb thiab hais kom RPM, rov qab siab nrog nws lub hauv paus siab, thiab cov ntaub ntawv thauj khoom lossis lub tswb.
- Kev txhaj tshuaj, cushion, ib feem thiab qhov hnyav khiav, cov ntaub ntawv kub thiab qhov muaj qhov rov qab muaj.
- Cov kev hloov pauv twb tau sim, lawv cov txiaj ntsig ntawm qhov zoo, thiab ib qho kev qhia txog kev hnav.
Rau commissioning, pom zoo rau cov resin, txhaj tshuaj, kev khiav hauj lwm qhov rais thiab tau ib feem zoo. Tom qab ntawd sib piv cov txheej txheem rov ua dua thiab lub sijhawm tag nrho lub voj voog. Ib qho kev sib cais sai dua plasticizing tsis txaus yog tias cov pwm tsim tawm tseem tos lossis cov khoom tsis raug tshuaj xyuas.

Xav tau ib tug ntsia hlau los yog chim lub tswv yim rau ib tug paub tseeb hais tias rov qab txwv?
Xa Nanhaiya cov duab kos thiab cov ntaub ntawv ua haujlwm, suav nrog qhov hloov pauv thiab dab tsi koj txoj kab xav tau kom ua tiav. Qhia rau peb seb koj puas tau rov qab ua lub luag haujlwm qub los yog npaj rau lwm yam khoom lossis lub voj voog uas yuav tsum tau ua.
Xa koj cov duab kos thiab txheej txheem cov ntaub ntawvSaib kev txhaj tshuaj molding screwsSib tham hauv WhatsApp
Zhoushan Nanhaiya Yas Machinery Co., Ltd.
Email:info@nhyscrew.com ib
Xov tooj:+86-13505809643| Txawb:+86-13587082002
Block C, No. 2 West Section, Xingzhou Avenue, Dinghai District, Zhoushan City, Zhejiang Province, Suav.
Hu rau Nanhaiya
Cov lus nug uas nquag nug
Dab tsi yog lub sijhawm txhaj tshuaj molding ntsia hlau rov qab?
Tsis muaj tus lej universal. Lub sij hawm rov qab nyob ntawm cov resin, txhaj tshuaj yuav tsum tau, ntsia hlau geometry, tshuab muaj peev xwm thiab cov chaw khiav hauj lwm. Sib piv nws nrog lub sij hawm muaj nyob rau hauv qhov tseeb tshuab ib ntus thiab nrog ib tug ruaj khov siv khiav siv tib yam khoom thiab txhaj tshuaj.
Puas ceev cov ntsia hlau rov qab ib txwm luv lub sij hawm voj voog?
Tsis yog. Nws shortens lub voj voog tsuas yog thaum rov qab ua tsis tiav yog ncua lub tshuab tso cai tom ntej. Yog tias qhov kev rov qab tau ua tiav nyob rau hauv lub qhov rais sib tshooj, ua kom nws nrawm dua tuaj yeem ua rau tag nrho lub sijhawm voj voog tsis hloov pauv.
Vim li cas cov ntsia hlau tig tab sis retract qeeb heev?
Xyuas seb cov resin ncav cuag cov ntsia hlau, seb puas rov qab hloov siab, thiab seb qhov ceev ceev tiag tiag puas phim cov lus txib. Pub bridging, inconsistent regrind, txheej txheem tej yam kev mob thiab hnav Cheebtsam yog tau ceg los soj ntsuam. Kev sib hloov ib leeg tsis ua pov thawj tias cov ntsia hlau xa khoom txaus.
Kuv puas yuav tsum nce RPM txhawm rau txhim kho kev rov qab qeeb?
Tsuas yog tom qab kuaj xyuas cov khoom noj, qhov tseeb ceev, rov qab siab thiab cov resin cov kev txwv. Txiav txim ib qho kev hloov pauv los ntawm kev ua kom zoo, qhov kub thiab txias thiab rov ua dua ntxiv nrog rau lub sijhawm rov qab los. Tsis txhob siv qhov nrawm dua los zais qhov tsis tuaj yeem noj lossis teeb meem hnav.
Puas yog lub nplhaib xau pov thawj tag nrho cov ntsia hlau tau hnav?
Tsis yog. Lub nplhaib sealing thiab ntsia hlau thoob conveying yog cov haujlwm sib txawv. Tshawb xyuas lub cushion lossis txhaj tshuaj hnyav sib txawv nrog lub tshuab chaw tsim khoom lub valve, thiab siv qhov ntsuas qhov ntsuas los tsim cov ntsia hlau thiab lub thoob coj.
Nanhaiya xav tau dab tsi los ntsuas qhov hloov pauv?
Xa lub tshuab qauv, ntsia hlau txoj kab uas hla thiab kos duab, qib resin thiab muab tub lim, regrind cov ntsiab lus, cov ntaub ntawv rov qab tiag tiag, ntsia hlau ceev thiab rov qab-siab qhov chaw, cov ntaub ntawv ntsuas kub, thiab kev ntsuas kev hnav. suav nrog lub voj voog uas yuav tsum tau muaj thiab cov txheej txheem zoo ib feem kom qhov kev hloov pauv muaj txoj haujlwm tau hais tseg.
Txuas ntxiv nrog rautxhaj tshuaj molding ntsia hlau chim xaiv phau ntawv qhia, los yog soj ntsuam covntsia hlau tip thiab check-ring hloov checklistyog tias cov pov thawj taw qhia rau lub rooj sib txoos pem hauv ntej.