Xov xwm

Parallel Twin Screw Extruder: Yuav Ua Li Cas Co-Rotating Compounding Ua Haujlwm

2026-08-14 0 Tso lus rau kuv


Teb ceev

Ib qho kev sib txuas ntxaib ntsia hlau extruder muaj ob qhov txuas txuas txuas txuas txuas txuas ua ke ua los ntawm cov khoom siv modular. Feem ntau yog co-rotating, khiav ntawm kev kub ceev rau intensive mixing - uas ua rau lawv tus qauv tshuab rau compounding, masterbatch, WPC thiab pelletizing. Tsis zoo li lub tshuab conical, cov ntsia hlau profile tuaj yeem rov tsim dua rau txhua qhov kev tsim tshiab.

Yog tias koj txoj haujlwm tab tom tig cov khoom xyaw rau hauv pellets - masterbatch, cov khoom sib xyaw ua ke, WPC, engineering plastics - qhov sib npaug ntxaib ntsia hlau extruder yuav luag yog lub tshuab koj xav tau. Nws lub ntsiab lus txhais tsis yog lub zog tab sisconfigurability: vim tias ob lub ntsia hlau thiab lub thoob yog tsim los ntawm cov qauv, ib lub tshuab tuaj yeem tsim kho kom haum rau daim ntawv qhia tom qab daim ntawv qhia. Cov lus qhia no suav nrog nws ua haujlwm li cas, vim li cas kev sib hloov dominates compounding, yuav ua li cas ntsia hlau configuration tiag tiag tsim, thiab yuav ua li cas loj lub tshuab rau koj cov zis.

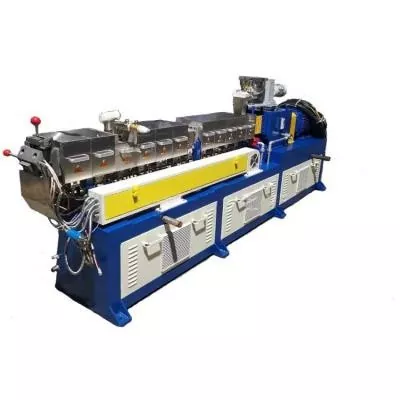
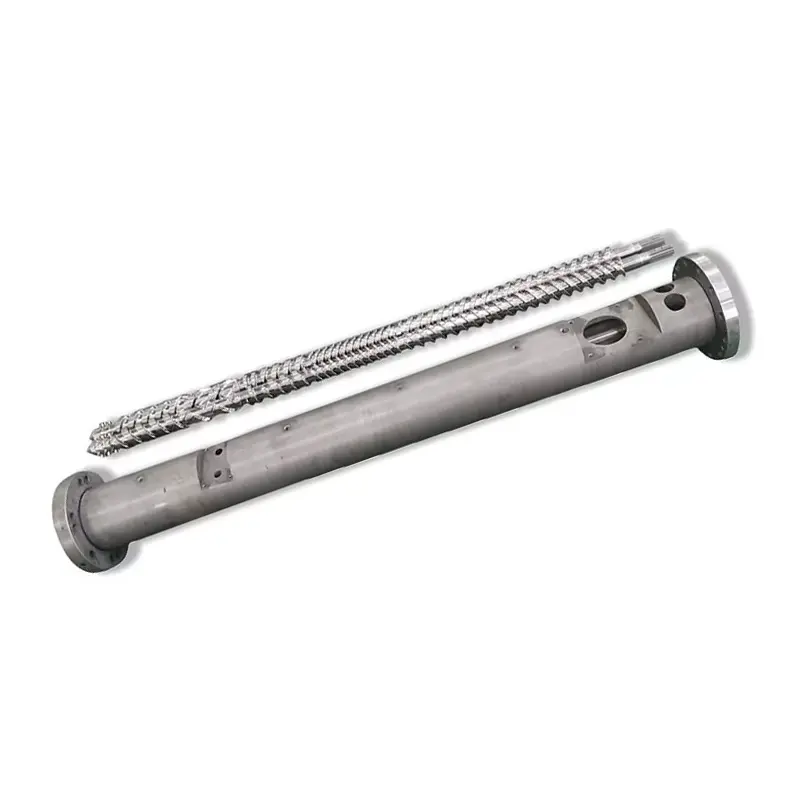
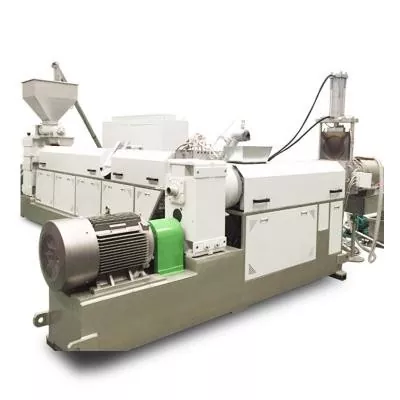
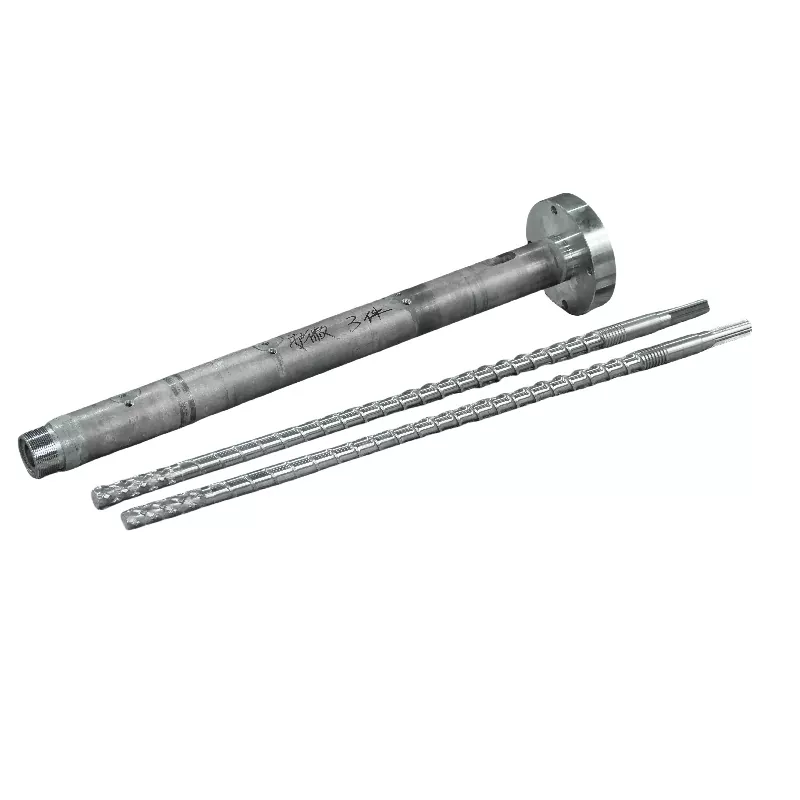
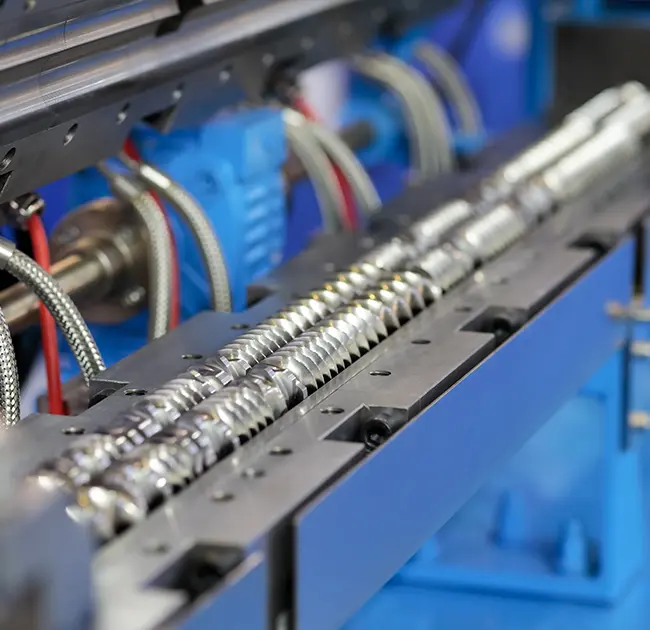
Parallel twin screw extruder pelletizing line by Nanhaiya

Yuav ua li cas ib tug parallel ntxaib ntsia hlau extruder ua haujlwm

Ob lub ntsia hlau ntawm txoj kab uas hla zoo ib yam khiav ntawm ib sab hauv daim duab-yim bore, intermeshing raws lawv tag nrho ntev. Cov khoom yog ntsuas nyob rau hauv - feem ntau yog los ntawm gravimetric los yog volumetric feeder es tsis yog dej nyab hopper - ces conveyed, melted, tov, vented thiab pumped mus rau tuag. Vim tias cov screws intermesh, cov khoom hloov pauv tau zoo los ntawm ib qho mus rau lwm qhov es tsis txhob raug rub los ntawm phab ntsa, uas ua rau lub tshuab nws cov zis ruaj khov thiab tus cwj pwm ntawm tus kheej so.

Lub sequence ntawm lub cev:

  1. Metered pub- feeders koob tshuaj resin, muab tub lim thiab additives ntawm qhov sib piv rau hauv seem pub. Sab feeders qhia iav fiber ntau los yog siab muab tub lim ntxiv downstream kom lawv tsis dhau-sheared.
  2. Melting- kneading blocks hloov txhua lub zog mus rau hauv tshav kub, melting lub polymer sai sai nyob rau hauv ib tug luv luv ntev.
  3. Sib tov- cov khoom faib kis tau cov khoom ntxiv sib npaug; Cov ntsiab lus dispersive rhuav tshem agglomerates. Qhov no yog qhov uas compound zoo yeej los yog poob.
  4. Devolatilisation- atmospheric thiab nqus vents rub tawm noo noo, monomer thiab volatiles.
  5. Metering & pelletizing- qhov kawg conveying seem tsim siab los ntawm cov tuag, ces ib tug strand los yog tuag-face pelletizer txiav cov yaj mus rau hauv granules.

Yog vim li cas compounding siv co-rotating tshuab

Ib qho kev sib txuas ntxaib ntsia hlau extruder tuaj yeem sib koom ua ke lossis counter-rotating, thiab qhov kev xaiv txhais lub tshuab ua cim.

Qhov xwm txheej Co-rotating thaum uas tig mus Counter-rotating thaum uas tig mus
Ntsia hlau tig Ob lub screws tig tib txoj kev Screws tig nyob rau hauv opposite lus qhia
Cwj pwm Self-wiping, high-shear mixing Calender zoo li, zoo conveying
Ntsia hlau ceev Siab - lub zog input tsav melting Lower - softer ntawm yaj
Lub zog Dispersive & distributive mixing, devolatilisation Tsis tshua muaj siab, qis shear
Hom kev siv Compounding, masterbatch, WPC, iav-fibre, recycling PVC yeeb nkab / profile, kub-rhiab heev thiab siab puv PVC

Nyob rau hauv kev xyaum, ib tug co-rotating ntxaib ntsia hlau extruder yog dab tsi cov neeg feem ntau txhais los ntawm "compounding extruder": tus kheej-so kev txiav txim tiv thaiv cov chaw tuag thiab cov khoom dai, thiab lub siab tshwj xeeb zog inputs melts thiab disperses sai. Counter-rotating parallel machines ciaj sia qhov twg shear yuav tsum nyob qis - feem ntau PVC. Rau ncaj qha PVC extrusion tshwj xeeb, aconical ntxaib ntsia hlau extruderfeem ntau yog cov lus teb zoo dua.

Ntsia hlau configuration: qhov tseeb specification

Nyob rau hauv ib lub tshuab ua ke, cov ntsia hlau tsis yog ib feem - nws yog ib pawg ntawm cov ntsiab lus tseem ceeb rau ntawm lub tog raj kheej. Covthaum uas tig mus twin ntsia hlau thiab chimyog li ntawd tau teev los ntawm nws lub caij sib lawv liag, tsis yog ib txoj kab uas hla. Lub tsev blocks:

  • Kev xa tawm cov ntsiab lus- pem hauv ntej-pitch flights uas thauj khoom; ntev pitch rau pub, luv suab rau siab tsim.
  • Kneading blocks- staggered discs uas yaj thiab sib tov. Lub stagger lub kaum sab xis teev tus cwj pwm: 30 ° thiab 45 ° rau pem hauv ntej rau kev faib khoom sib xyaw, 90 ° nruab nrab rau kev sib cais hnyav, thim rov qab rau qhov siab tshaj plaws shear thiab tag nrho cov yaj.
  • Rov qab (sab laug-tes) cov ntsiab lus- tsim lub foob pob zeb kom lub tshuab nqus tsev tuaj yeem ua haujlwm, thiab tsa lub sijhawm nyob hauv zos.
  • Kev sib xyaw ua ke- toothed los yog slotted designs rau maj mam distributive mixing tsis dhau shear.
  • Cov seem- pub, kaw, sab-feed, atmospheric-vent thiab nqus-vents bolted nyob rau hauv qhov kev txiav txim ntawm daim ntawv qhia xav tau.
General kev lag luam ceeb toom:co-rotating compounding tshuab feem ntau ua nyob rau hauv L / D ratios nyob ib ncig ntawm 32: 1 mus rau 48: 1, nrog ntev ntev siv thaum ib daim ntawv qhia xav tau kev pub noj sab ntxiv rau ntau yam sib tov thiab venting theem. Paub meej tias L / D thiab cov txheej txheem ib ntus tawm tsam koj qhov kev tsim tshwj xeeb.
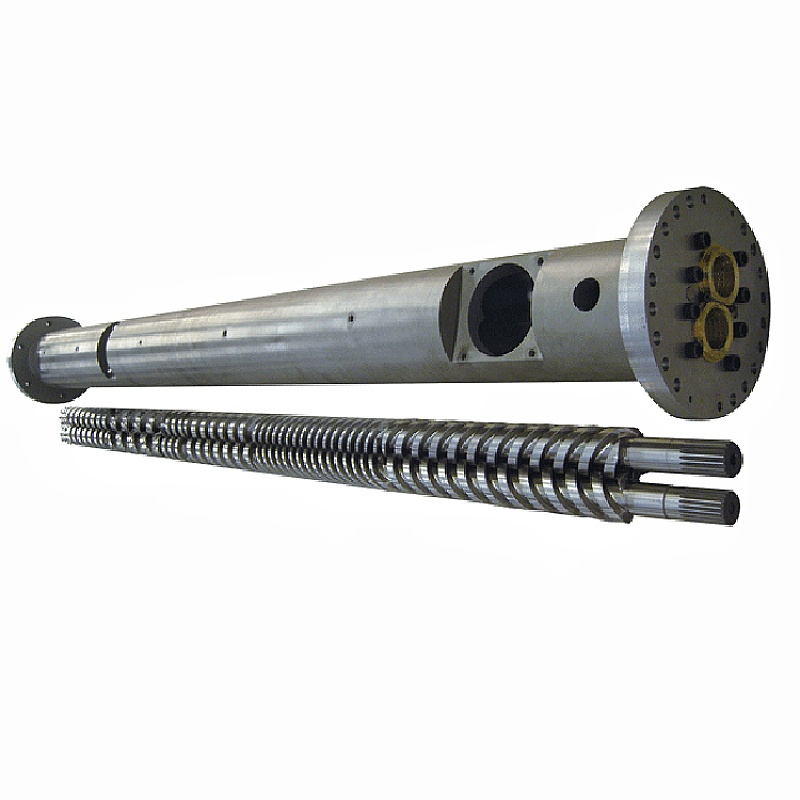
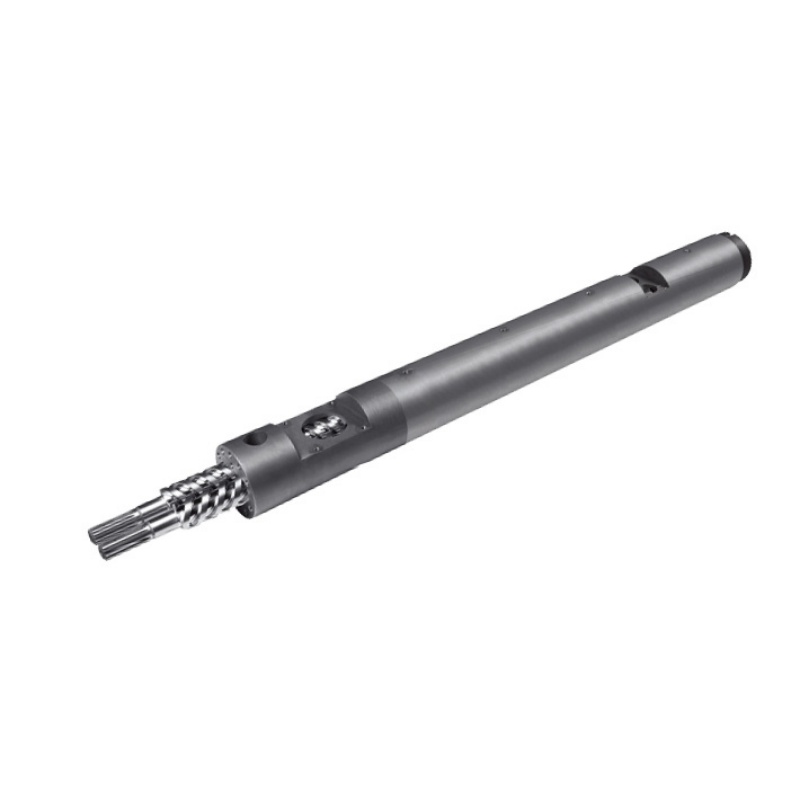
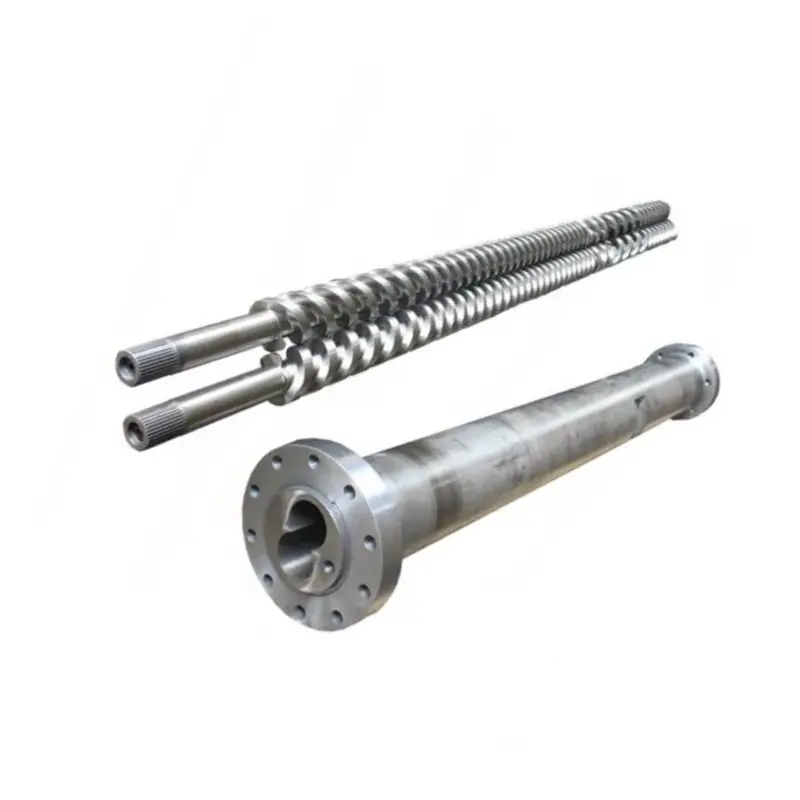
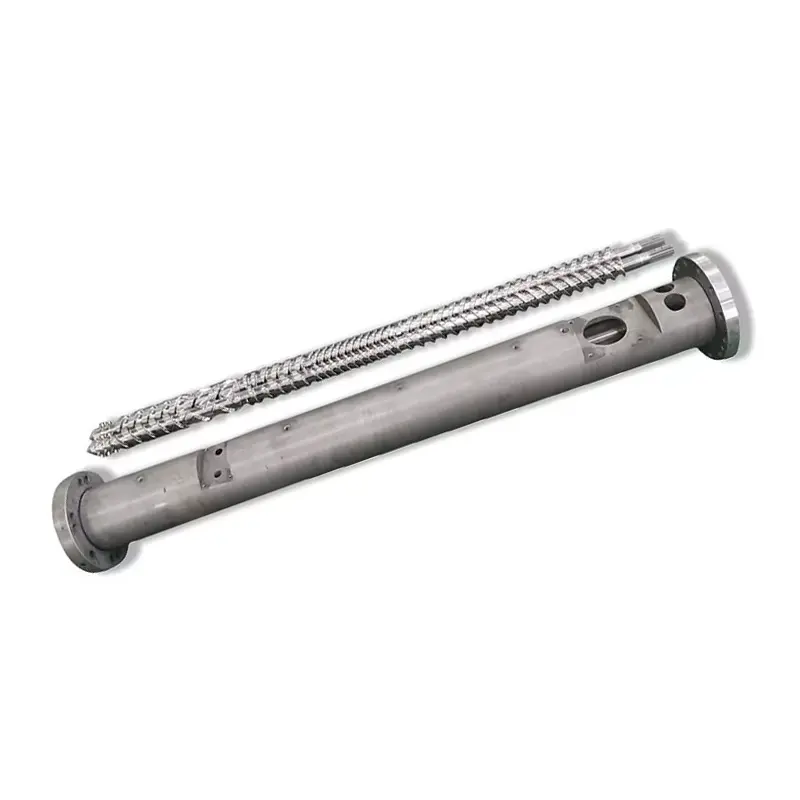
Segmented parallel twin screw elements for a compounding extruder

Lub extruder tsuas yog ib feem ntawm txoj kab

Ib qho sib npaug ntxaib ntsia hlau extruder tsis tshua ua haujlwm ib leeg. Ib txoj kab sib xyaw ua tiav feem ntau suav nrog:

  • Feeders- gravimetric poob-hauv-qhov hnyav units rau kev noj zaub mov kom raug.
  • Sab feeder- qhia txog iav fiber ntau los yog hnyav muab tub lim downstream los tiv thaiv fiber ntau ntev.
  • Lub tshuab nqus tsev- tshem tawm noo noo thiab volatiles los ntawm yaj.
  • Qhuav lim- screen changer kom ntes cov kab mob sib kis, tseem ceeb ntawm cov khoom noj rov qab.
  • Pelletizer- strand, dej-ntiv nplhaib los yog tuag-ntsej muag (underwater) txiav, xaiv los ntawm cov khoom.
  • Txias & ziab- da dej los yog cua txias ntxiv rau lub tshuab ziab khaub ncaws ua ntej ntim.

Nanhaiya muab cov extruder ib leeg lossis ua tiavthaum uas tig mus ntxaib ntsia hlau pelletizing kab, zoo lilwm yam extruder tshuabrau ib leeg ntsia hlau thiab conical layouts.

Sizing thiab tso zis

Parallel cov cav tov muaj npe los ntawm cov ntsia hlau taub - lub tshuab 65 hli muaj ob lub qhov 65 hli. Cov zis nce nrog txoj kab uas hla, ntsia hlau ceev thiab torque, tab sis daim ntawv qhia teeb lub qab nthab tiag tiag: ib qho kev sib xyaw ua ke uas xav tau kev sib cais hnyav yuav khiav qeeb dua li cov xim yooj yim masterbatch ntawm tib lub tshuab.

Dab tsi teev cov zis Vim li cas thiaj tseem ceeb
Ntsia hlau txoj kab uas hla Lub hauv paus muaj peev xwm ntawm lub tshuab - yuav tsum phim koj lub hom phiaj throughput band
Screw ceev (rpm) Kev nrawm dua nqa cov zis tab sis kuj shear thiab yaj kub
Torque ceev Muaj torque rau ib chav tsev ntim - qhov txwv ntawm cov zaub mov uas muaj puv heev
L/D ratio Ntev ntev tso cai rau sab pub mis, sib xyaw ua ke ntau dua thiab ua kom cua zoo dua
Kev tsim qauv Filler qib thiab dispersion nyuaj feem ntau khi ua ntej lub tshuab ua
Downstream peev Cov pelletizer thiab cua txias yuav tsum khaws cia los yog lawv dhau los ua lub fwj

Cov tswv yim mus kom ze: qhia peb cov compound, qib muab tub lim thiab kg / h koj xav tau, thiab peb yuav loj lub tshuab thiab tsim lub caij nyob ib ncig ntawm nws - tsis yog muag koj ib txoj kab uas hla thiab vam tias daim ntawv qhia haum.

Dab tsi parallel ntxaib ntsia hlau extruders ua

  • Masterbatch- xim, muab tub lim thiab additive concentrates.
  • Filled compounds- CaCO₃, talc thiab mineral-filled PP thiab PE.
  • Iav-fiber reinforced engineering plastics- PA, PBT thiab PP nrog sab-fed fiber.
  • WPC pellets- wood-fibre compounds rau decking thiab panels.
  • PS ua npuas ncauj— saib pebPS ua npuas ncauj parallel ntxaib ntsia hlau.
  • Aluminium-yas vaj huam sib luag— saibaluminium-yas phaj parallel ntxaib ntsia hlau.
  • Rov ua dua- reprocessing thiab kho dua tshiab cov khoom tom qab kev lag luam.

Parallel lossis conical tshuab?

Lus nug Parallel ntxaib ntsia hlau extruder Conical ntxaib ntsia hlau extruder
Cov zis yog dab tsi? Pellet los yog compound Ib tug tiav profile, yeeb nkab los yog board
Ntsia hlau Txoj kab uas hla tsis tu ncua, cov ntsiab lus modular Tapered, tsau geometry ib qhov loj me
Daim ntawv qhia hloov Rebuild lub ntsia hlau profile Hloov cov cuab yeej downstream
Pub Metered feeders, feem ntau sab pub Forced (crammer) feeder rau PVC hmoov
Shear Siab - qhov ntawd yog qhov taw tes Tsawg thiab maj mam rau qhov kub-sensitive PVC

Tsis paub meej qhov twg haum? Pib los ntawm peb qhov davntxaib ntsia hlau extruder qhia, uas piv ob tsev neeg ib sab ntawm ib sab.

Screw thiab chim: qhov uas hnav

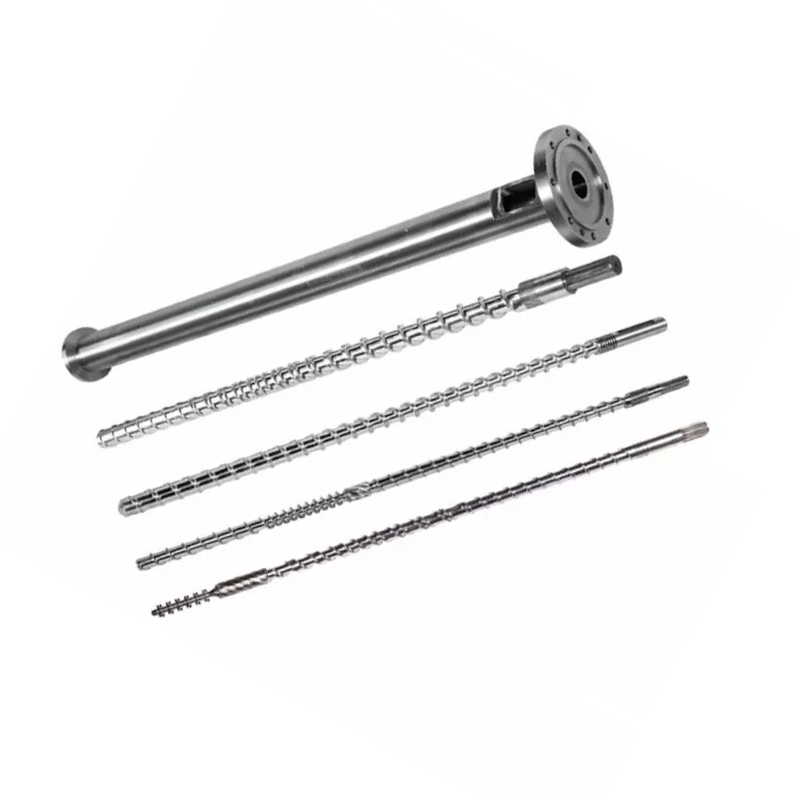
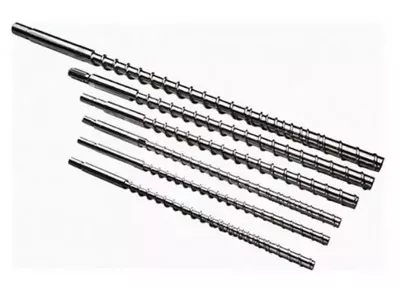
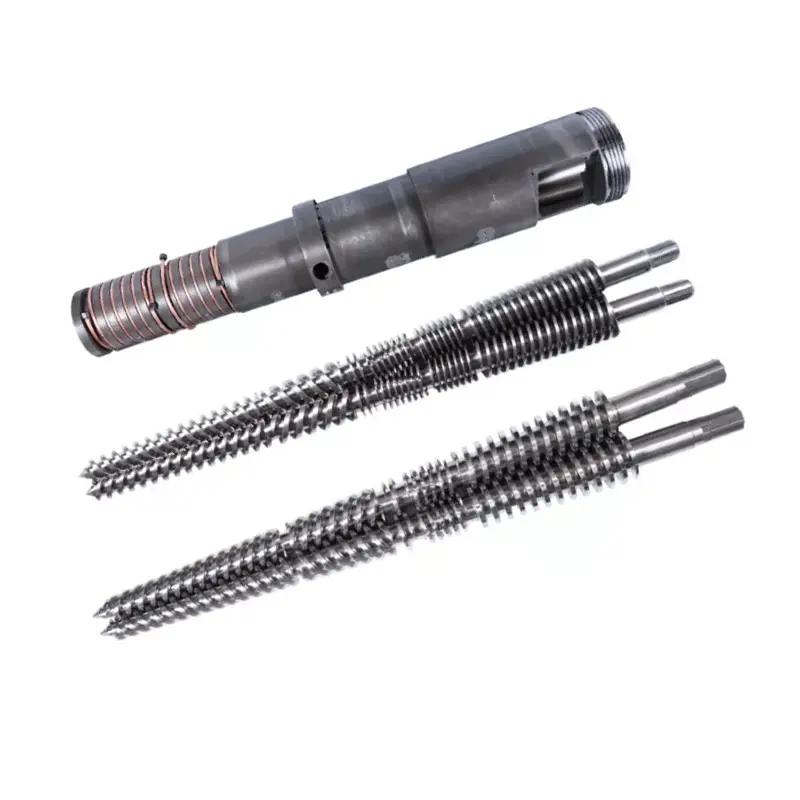
Compounding yog nyuaj rau steel. Cov iav fiber ntau, ntxhia muab tub lim thiab siab carbonate loadings abrade ob lub davhlau cov lus qhia thiab lub bore, thiab ib lub caij hnav ib ntus poob kev sib xyaw ua haujlwm ntev ua ntej lub tshuab nres. Yog vim li cas tusthaum uas tig mus twin ntsia hlau chimthiab nws cov ntsiab lus yuav tsum tau teev tseg rau kev puas tsuaj koj daim ntawv qhia tiag tiag tsim.

Nanhaiya tsim cov ntsia hlau sib txuas thiab cov thoob los ntawm 38CrMoAlA nitrided steel, W6Mo5Cr4V2 lossis HIP hmoov hlau, tuav kom ua siab ntev ntawm ± 0.01 hli nrog qhov ncaj ntawm 0.015 hli / m. Rau abrasive tebchaw peb tsuag ib tug tungsten-ntxiv hard alloy uas ncav cuag62 HRCsab hauv lub bore - tawm tsam ib qho 58 HRC - nrog 2.0-3.0 mm alloy txheej. Cov qauv tsim qauv kuj tseem pab ua lag luam: koj tsuas yog hloov cov khoom hnav, tsis yog tag nrho cov ntsia hlau. Saib peb qhov kev sib piv ntawm abimetallic vs nitrided ntsia hlau chim, thiab pebkhoom seemntau.

Cov lus nug uas nquag nug

Dab tsi yog qhov parallel ntxaib ntsia hlau extruder?

Nws yog ib qho extruder nrog ob qhov txuas txuas txuas txuas txuas nrog cov ntsia hlau ua los ntawm cov ntsiab lus modular ntawm splined shafts. Feem ntau yog co-rotating thiab yog siv rau compounding, masterbatch, WPC thiab pelletizing, vim hais tias cov ntsia hlau profile yuav rebuilt rau txhua formulation.

Dab tsi yog co-rotating ntxaib ntsia hlau extruder siv rau?

Compounding thiab pelletizing saum toj no tag nrho - masterbatch, ntim thiab iav-fibre reinforced compounds, WPC thiab recycling. Tus kheej-wiping, high-shear nkaus muab muaj zog dispersive thiab distributive sib tov ntxiv rau devolatilisation zoo.

Co-rotating lossis counter-rotating - uas zoo dua?

Tsis yog universally. Co-rotating suits compounding thiab sib tov ntawm cov ntsia hlau ceev ceev. Counter-rotating muab softer, zoo conveying thiab suits PVC thiab kub-rhiab heev, ua hauj lwm zoo heev. Txuas lub tshuab rau txoj haujlwm, tsis yog rov qab.

Parallel los yog conical ntxaib ntsia hlau extruder?

Xaiv thaum uas tig mus thaum cov zis yog pellets los yog ib tug compound thiab koj xav tau reconfigurable sib tov. Xaiv conical thaum extrudate nws tus kheej yog koj cov khoom - PVC yeeb nkab, profile, board los yog ntawv - qhov twg muaj zog noj thiab maj mam compression tseem ceeb dua.

Dab tsi yog kneading blocks thiab vim li cas lawv tseem ceeb?

Kneading blocks yog staggered disc ntsiab uas yaj thiab sib tov cov compound. Lub stagger lub kaum sab xis teev cov nyhuv: rau pem hauv ntej cov ces kaum muab faib sib xyaw, nruab nrab 90 ° muab intensive dispersion, thiab cov ntsiab lus thim rov qab tsim lub yaj foob rau lub tshuab nqus tsev.

Yuav ua li cas yog ib tug parallel ntxaib ntsia hlau extruder loj?

Los ntawm txoj kab uas hla, ntsia hlau ceev, muaj torque thiab L / D piv - tab sis cov formulation feem ntau teev qhov kev txwv tiag. Cov zaub mov ua kom puv lossis nyuaj-rau-disperse khiav qeeb dua li yooj yim masterbatch ntawm tib lub tshuab, thiab cov pelletizer yuav tsum khaws cia.

Dab tsi yog side feeder rau?

Ib sab feeder qhia cov iav fiber ntau los yog cov khoom ntim siab loads downstream ntawm melting seem. Ntxiv fiber ntau tom qab cov polymer tau yaj yuav tiv thaiv fiber ntau ntev thiab tsis txhob muaj cov shear ntau dhau uas lub ntsiab pub ntxiv yuav ua rau.

Ntev npaum li cas cov screws thiab cov thoob kav ntev npaum li cas?

Nws nyob ntawm kev puas tsuaj. iav fiber ntau thiab ntxhia muab tub lim hnav cov ntsiab lus ceev tshaj plaws. Ib qho bimetallic nto nrog 2.0-3.0 hli alloy txheej ntawm mus txog 62 HRC txuas lub neej zoo, thiab cov qauv tsim cia koj hloov cov khoom hnav xwb es tsis yog tag nrho cov ntsia hlau.

Cov khoom lag luam cuam tshuam los ntawm peb lub Hoobkas

Tau txais qhov sib npaug ntxaib ntsia hlau extruder ua nyob ib ncig ntawm koj daim ntawv qhia

Qhia rau peb koj qhov kev sib xyaw ua ke, qib muab tub lim thiab lub hom phiaj kg / h - peb cov kws tsim khoom yuav loj lub tshuab thiab tsim cov ntsiab lus ntawm cov ntsia hlau kom phim, ces hais cov extruder ib leeg los yog ua tiav pelletizing kab.

Tau txais cov lus hais hauv 12 teev →
Nanhaiya (Zhoushan) Yas Machinery · 500+ cov neeg siv khoom thoob ntiaj teb ·thaum uas tig mus & conicalntxaib ntsia hlau systems,extruder tshuab & khoom seem
Cov xov xwm ntsig txog
Tso lus rau kuv
X
Peb siv cov ncuav qab zib los muab koj cov kev tshawb fawb zoo dua, txheeb xyuas qhov chaw khiav tsheb thiab kho cov ntsiab lus tus kheej. Los ntawm kev siv lub xaib no, koj pom zoo rau peb siv cov ncuav qab zib. Txoj Cai Tswjfwm Ntiag Tug
Tsis lees paubTxais